
PROCESS FLOW CHART OF SEAMLESS STAINLESS STEEL PIPES
Step-by-Step Stainless Steel Seamless Pipe Production Process
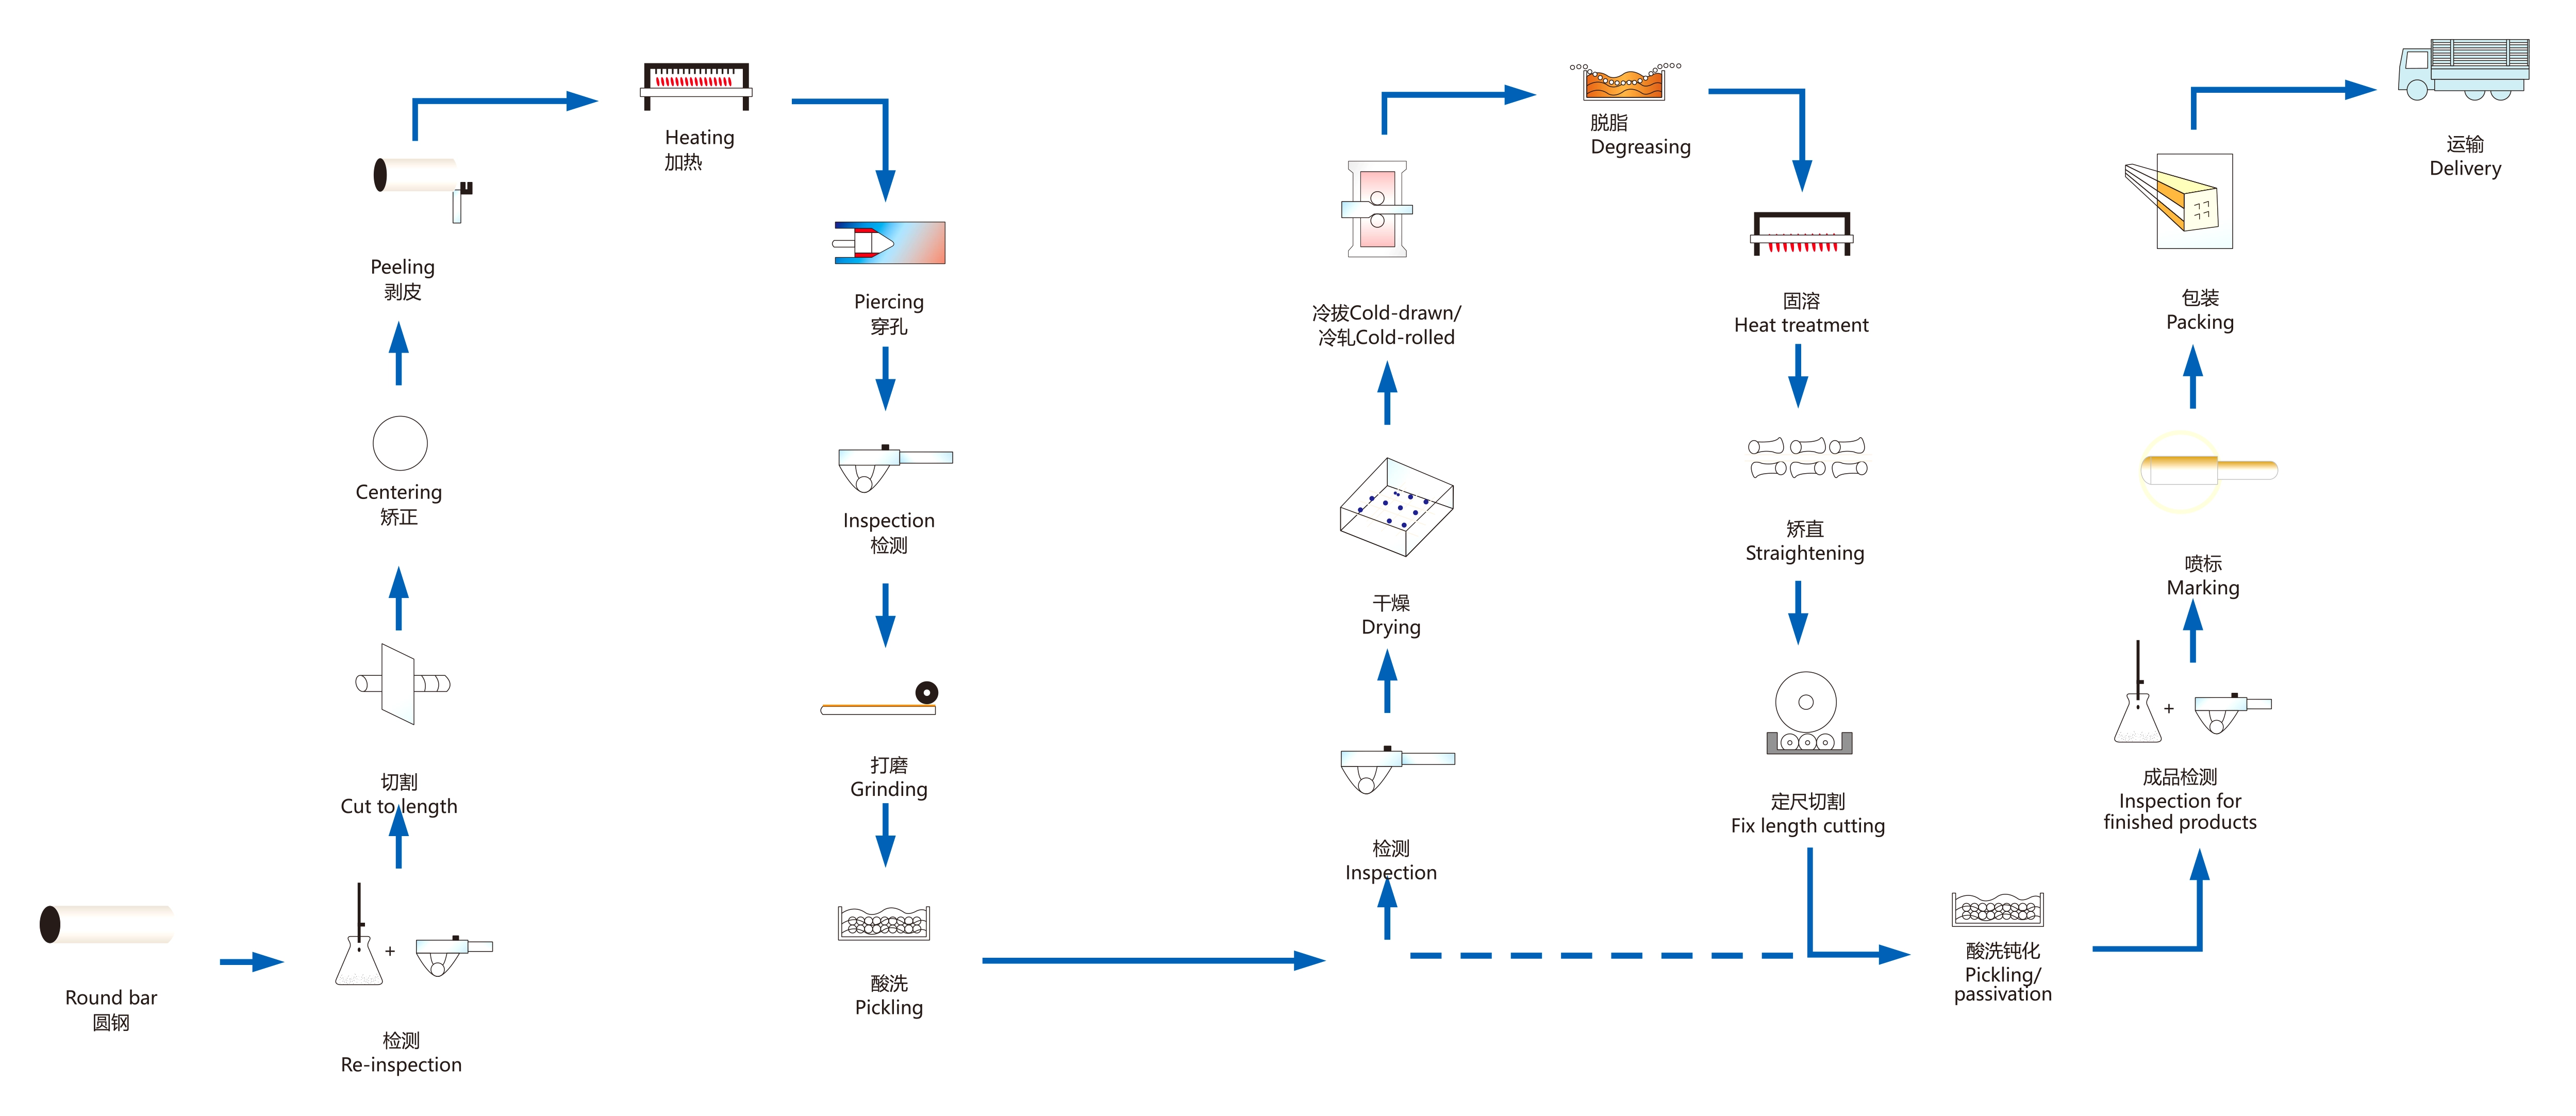
All the steps have been explained in detail below:
1. Round Bar Selection
This is the first step towards production seamless products at Xintongda. We select a strong round bar or a billet of the required grade. As we have to produce the products without any weld seams, we select the best round bars.
2. Re-inspection
Once we select the round bar, we send it for re-inspection to check the quality and purity of the bar.
3. Cut to Length
The round bar is then cut to a specific length or the maximum length as desired.
4. Centering
Centering is a step in which the bar’s axis is aligned with the plug before it is pierced. This step is crucial as the plug (the internal diameter of the pipe/ tube) should accurately correspond to the bar’s central axis.
5. Peeling
Peeling basically means to remove the outer surface of the bar or billet to avoid surface defects. In this process, cracks, scale, inclusions, or decarburised layers are eliminated from the billet.
6. Heating
The peeled bars are then sent for heating in a furnace. This process makes the bars soft, so that they do not crack when pierced.
7. Piercing
Piercing involves converting the round bar into a hollow shell by creating a hole. This is one of the most important steps.
8. Inspection
Once pierced, the hollow shells undergo inspection to check dimensional accuracy and defects. This step helps us to discard shells with issues and save time.
9. Grinding
This step removes surface irregularities and excess material by grinding. It is a key step to improve the surface finish and dimensional precision.
10. Pickling
Pickling involves treating the surface of the hollow shell with an acid solution to get rid of oxidation, scaling, rust, contaminants, and other impurities. This step makes the shell chemically prepared.
11. Inspection (Post-Pickling)
The hollow shell is again inspected after pickling for surface and dimensional quality. This step confirms that the earlier steps were successful.
12. Drying
Drying mainly refers to the process of removing moisture, coatings, or other unwanted residues that were left due to pickling or washing. Moisture can lead to corrosion, and hence drying is an important step.
13. Cold Drawing / Cold Rolling
In cold drawing, the hollow shell is pulled through a die over a mandrel to reduce its diameter, wall thickness, and improve its dimensional accuracy and surface finish. Cold rolling, on the other hand, is a similar process where the hollow shell is rolled on a two-roll mill at room temperature. Both processes provide similar results.
14. Degreasing
Degreasing is a cleaning process where lubricants, oils, greases, and fatty acids used during cold working are removed to make the surface clean.
15. Heat Treatment
The heat treatment step involves heating and cooling the hollow shell under controlled conditions. This step modifies the internal microstructure of the pipe/ tube and improves its mechanical properties.
16. Straightening
There is a chance that the hollow shell might bend, twist, or deform during cold rolling. In straightening, an external force is applied to straighten and remove such deforms. The product achieves proper alignment due to this step.
17. Fixed Length Cutting
The straightened pipe/ tube is cut to a length specified by the consumer or according to the application.
18. Pickling/ Passivation
Once the product is cut to a fixed length, it again undergoes pickling to remove any oxides or to improve its corrosion resistance. In passivation, the surface of the pipe/ tube is treated with an oxidant. This oxidation forms an oxide layer, which resists oxidation.
19. Inspection for Finished Products
After pickling, the product is sent for a final inspection to check dimensions, surface quality, and compliance with the international ASTM standards.
20. Marking
Once inspected, all the products are marked with relevant details, like grade, size, thickness, outer diameter, heat number, etc. Due to this, all our products are easily traceable.